Quality Control
Valve Quality Control Based on Product- and Order-specific Evidence
Quality control becomes useful when inspection and test requirements are tied to an exact valve, purchase order and acceptance basis. Lianggong’s documented metrology and test imagery supports facility context; it does not assign a result to an unverified product.
Project focus: valve quality control. Use the product, industry and resource links below to continue from this page’s defined scope.
Buyer decision
How to make valve quality evidence auditable
Inspection only helps procurement when each result names the valve, acceptance basis, method, stage and responsible record. Begin with the offered product and project requirements.
Define the inspection scope
Link characteristics, acceptance criteria, method, stage and responsibility to the offered product.
Verify the test basis
Pressure, functional or other tests must state procedure, conditions and record identity.
Close the document package
Drawings, materials, inspections, tests, deviations and release records should form one traceable file.
Information framework
Define inspection, testing and release requirements
Put material checks, in-process inspection, applicable tests and final release into the RFQ or inspection plan. Their criteria and witness points must be agreed for the exact configuration.
| Decision area | Buyer inputs | Why it matters |
|---|---|---|
| Incoming and material review | Identity, specification, records and condition | Supports input traceability |
| In-process inspection | Dimensions, workmanship and defined process checkpoints | Detects variation before final assembly |
| Testing | Applicable pressure, function or performance procedure and acceptance | Generates configuration-specific evidence |
| Final release | Approved product identity, deviations and document register | Aligns shipment with the purchase order |
Documented visual evidence
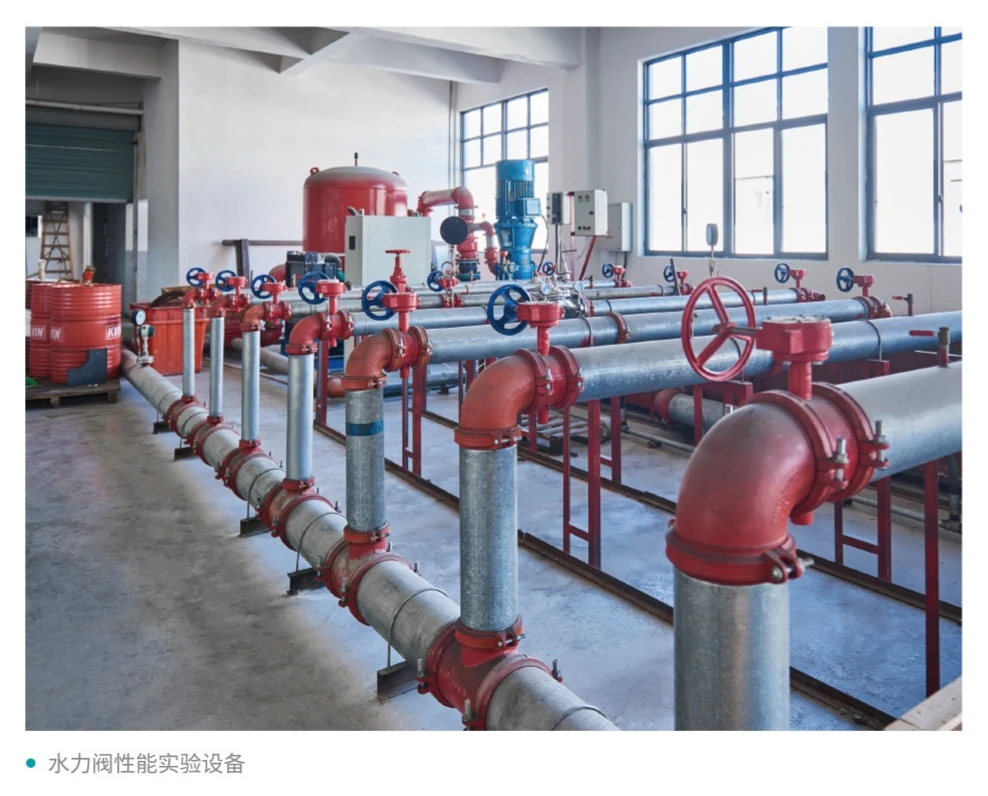
See documented measurement and test context
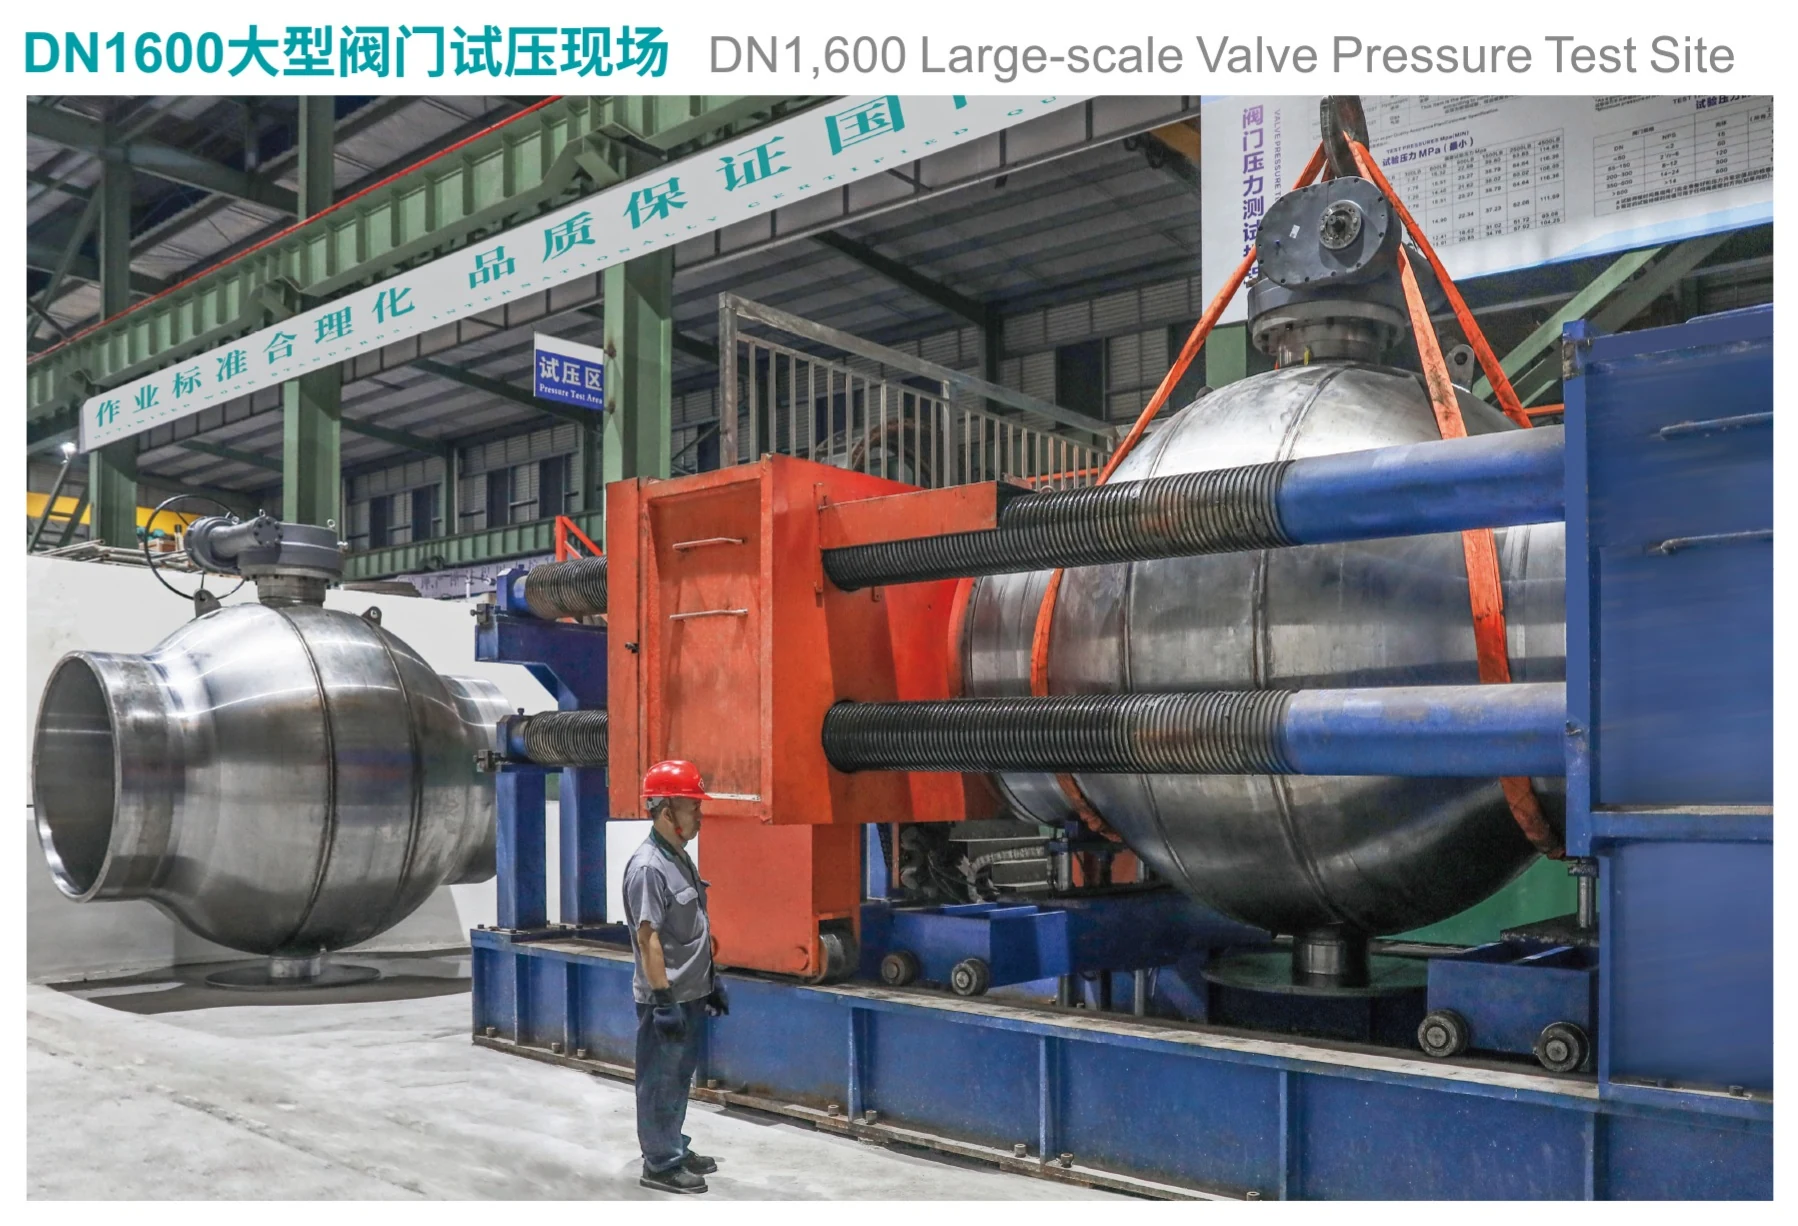
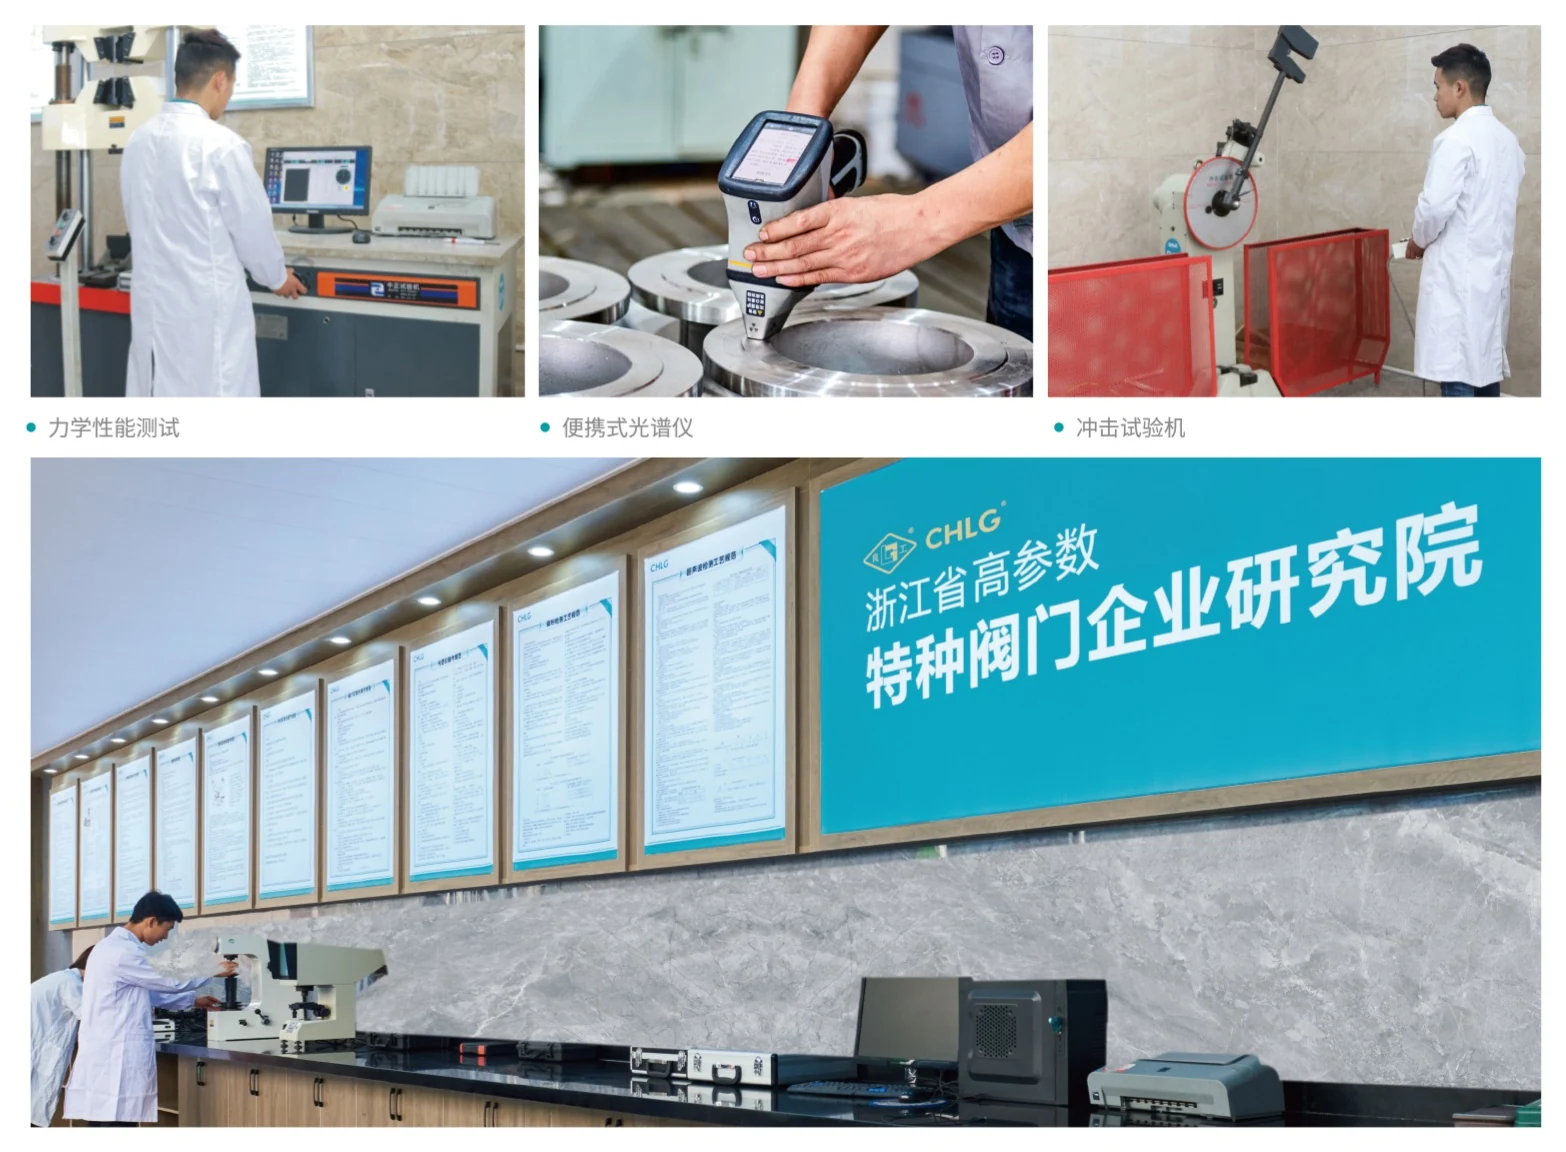
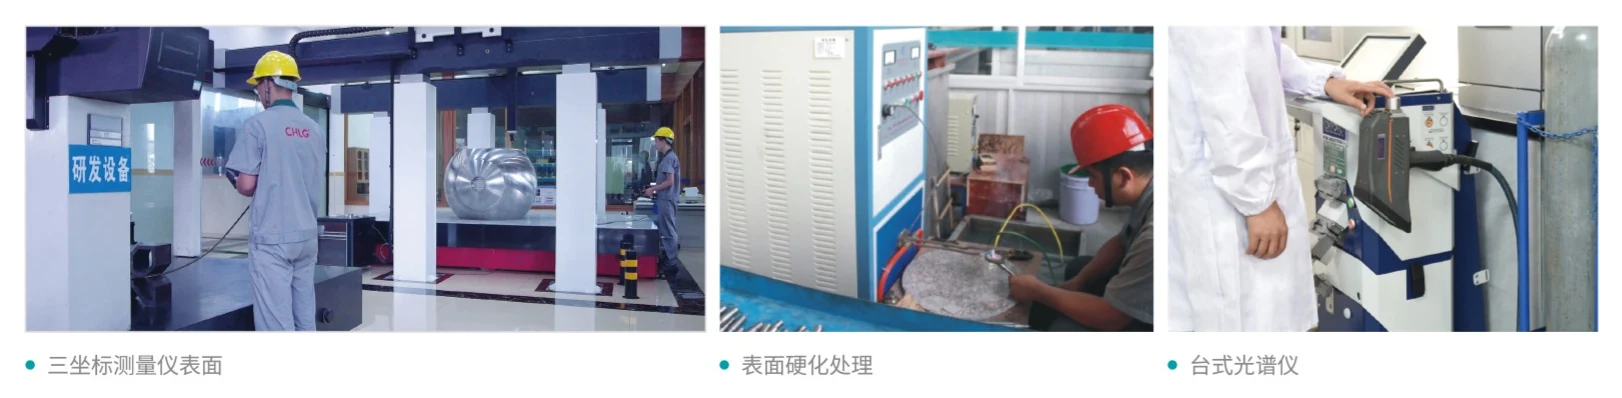
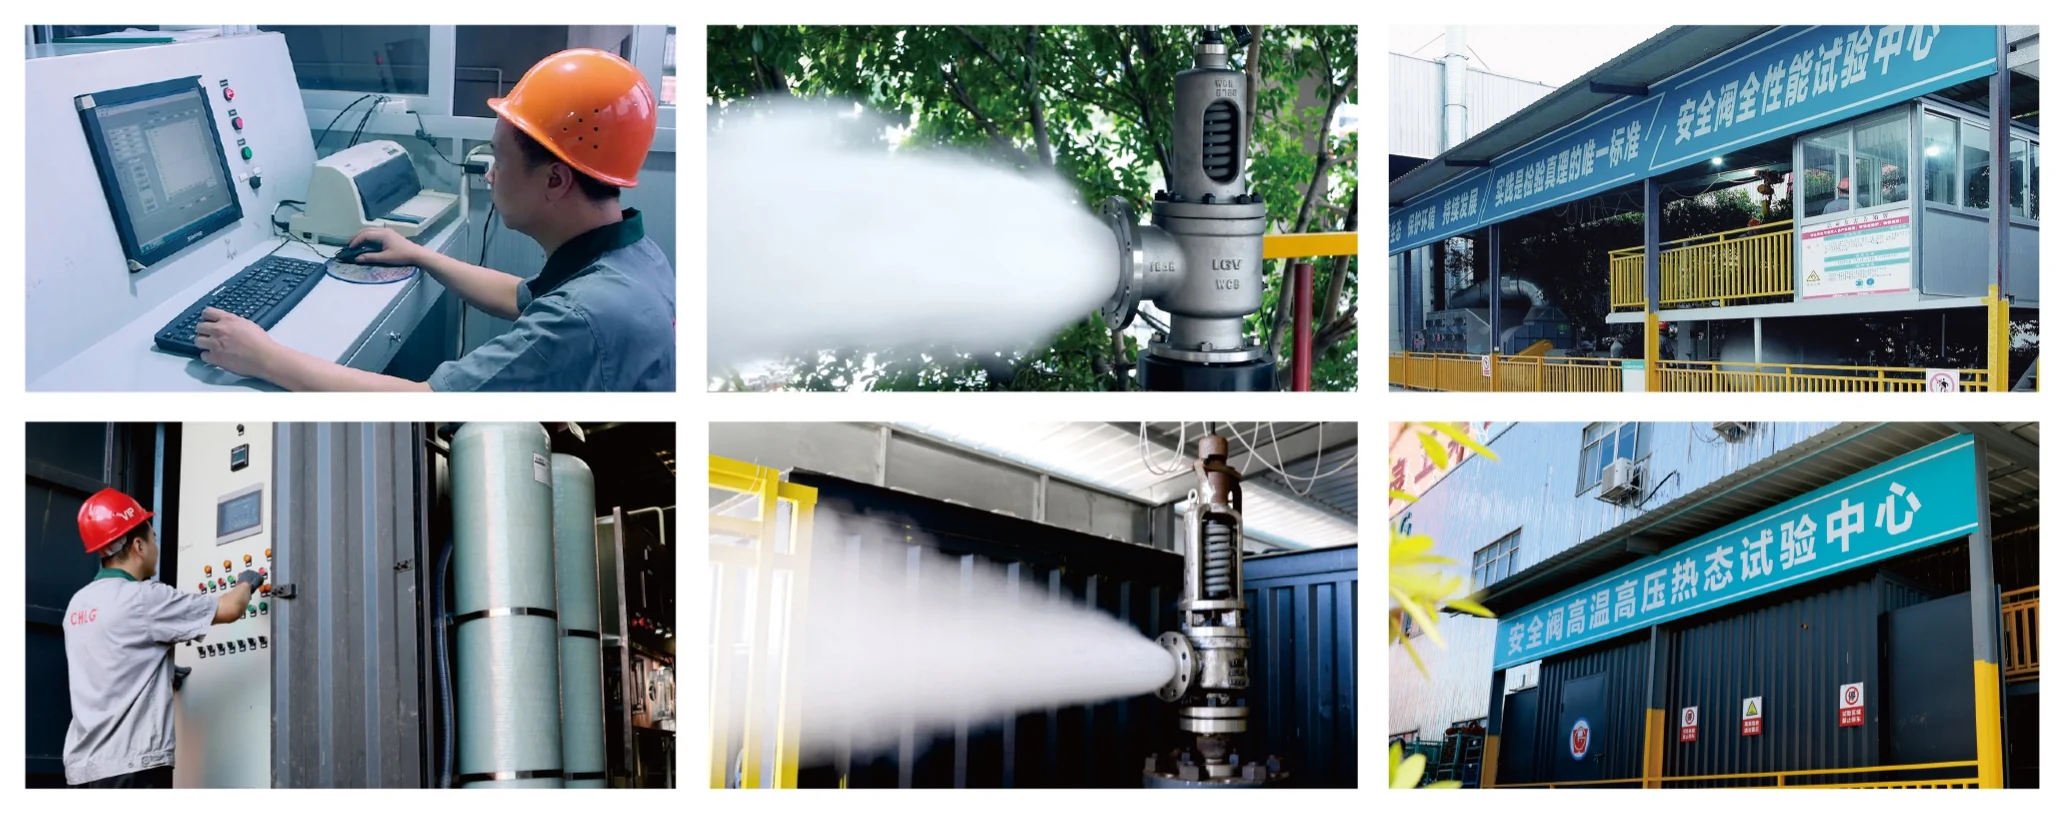
The images show measurement and test context. They do not prove that an unnamed valve passed a test or that a certificate covers a proposed model.
Evidence and claim limits
Match every quality claim to a valve and order
A quality statement becomes useful when it points to the identified valve, test or inspection procedure, acceptance criterion, result and revision-controlled record.
Verified public context
For buyers using the Quality Control page, use only documented page and product identities, mapped assets and facts supported by the current source files.
Configuration-specific facts
When using Quality Control for project handoff, keep materials, pressure, temperature, dimensions, standards and tests tied to the exact offered product.
Independent proof required
For the next action from Quality Control, certificates, named customers, projects, shipments and quantitative claims require their own current records.
Quality and trust risks
Avoid unsupported test and certification claims
Do not turn laboratory imagery into a passed test, apply a company-level certificate to every product, or imply 100% inspection without a defined documented scope.
- Using laboratory photos as a product test certificate
- Saying 100% tested without a defined scope
- Publishing standards or pass criteria not tied to the order
- Losing traceability between valve tag and record
- Confusing company capability with a specific inspection result
Practical next step
Agree hold points and deliverables before production
State required checks, test conditions, witness points, deviations and deliverables before the order proceeds. This keeps expectations clear for engineering and procurement.
1. Name the decision
State what must be selected, verified, quoted or documented.
2. Attach the inputs
Share relevant datasheets, schedules, drawings and project specifications.
3. Identify unknowns
Mark missing fields and responsibility instead of inserting assumed values.
4. Confirm the output
Agree the required quotation, submittal, record or follow-up route.
Practical buyer guidance
What a buyer should expect in the quality file
A reviewable quality package ties every drawing, material record, inspection result, test result and approved deviation to the correct valve and purchase order.
Acceptance starts in the RFQ
A quality plan works when characteristics, methods, stages, responsibilities and acceptance criteria are agreed before production. Adding requirements after manufacture may create gaps that photographs or generic certificates cannot close.
Records need product identity
A pressure, dimensional or material record is meaningful only when it connects to the exact valve, tag, serial/lot basis, procedure and purchase order. An unlabeled test image cannot provide that traceability.
Deviations must remain visible
Nonconformances, concessions and approved exceptions should be controlled with the same discipline as passing results. Hiding an exception behind a generic quality statement weakens both engineering review and commercial accountability.
Certificates have boundaries
Every certificate should be checked for issuer, validity, standard, product scope and relationship to the offered configuration. A company-level document cannot automatically prove a product-level requirement.
Decision record
Track open quality documents and exceptions
For each missing record, identify the valve tag or product, document type, required revision, acceptance basis and responsible party.
Selected route
Record the product, industry, resource or contact owner that now holds the decision.
Open questions
When using Quality Control for project handoff, list missing technical, commercial, evidence and responsibility items with an owner for follow-up.
Required deliverable
For buyers using the Quality Control page, define whether the next output is a shortlist, clarification, quotation, drawing, datasheet, inspection plan or document package.
Buyer questions
Questions about inspection and test records
These answers explain how to request and evaluate records; they do not claim an unnamed catalog item has passed a particular test.
What quality documents can be requested?
Specify the drawings, material records, inspection reports, test records, deviations and certificates required for the order.
Do facility images prove a valve passed testing?
No. A result requires an identified product, procedure, conditions and signed record.
When should inspection requirements be agreed?
Define them in the RFQ and purchase order before production and hold-point scheduling.
Choose the next evidence
Move from quality principles to a verifiable valve file
Product identity, manufacturing route and document revision must remain linked. Use these pages to prepare a specific evidence request.
Identify the exact product
Begin with the category, series or catalog identity being offered.
Review manufacturing context
Understand where material, process and assembly checks may be required.
Check document availability
Request the drawing, datasheet, material and test records relevant to the offer.
State acceptance in the RFQ
List standards, inspections, witness points, deviations and deliverables.
Inspection evidence
Testing facilities are visible; order records remain configuration specific
The catalog shows dedicated testing and inspection areas plus process-inspection scenes. These images support the existence of quality-control infrastructure, but they do not by themselves prove a product certificate, test value or third-party approval for a specific order.
Testing and inspection centre
The 2026 catalog documents a dedicated testing and inspection centre.
Process inspection
The catalog includes process-detection and inspection scenes across manufacturing operations.
Request the exact record set
For an RFQ, define the applicable standard, inspection plan, pressure-test scope, material records and certificate requirements.
Evidence source: Lianggong Valve Product Catalog EN, issued 30 June 2026, testing and process-detection pages 24–25
Technical and commercial contact
Request an order-specific quality review
Provide the offered product identity and inspection requirements so the applicable quality evidence can be checked against the actual order.